
Infrastructure
The melting shop, the radial forge, the presses and the machine shop, with the working capacity of each.
- 5,000M.T.
- Largest press
- 1400°C
- Reheating to
- 90+
- CNC machines
Forging
Three forging routes. The route for a job is decided by its shape and diameter.
-
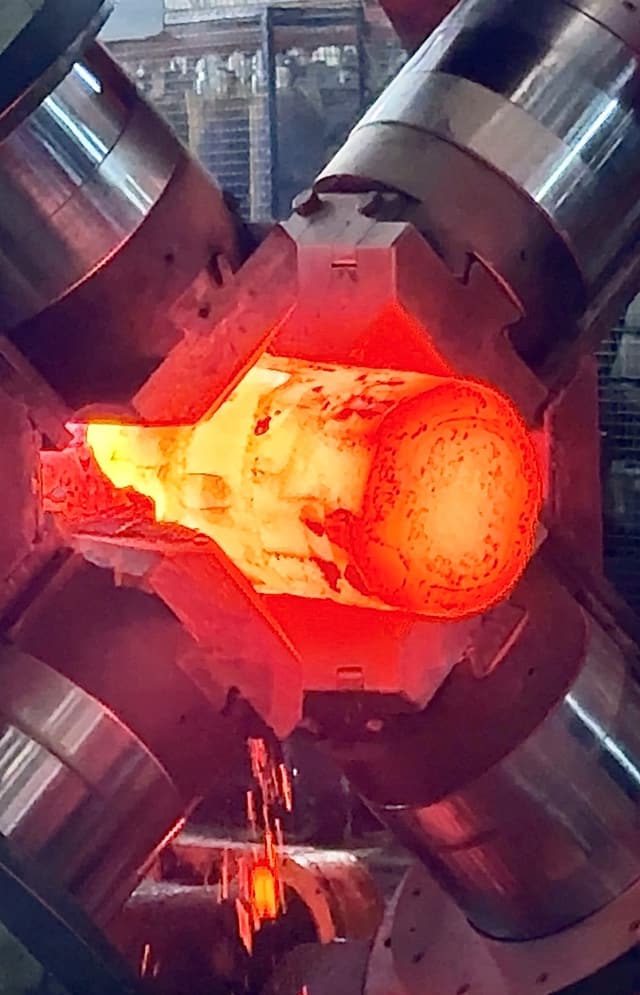
Hydraulic radial forge
Up to 200 forging strokes per minute
Four opposed cylinders in an X, closing in synchronised strokes. Two manipulators grip, position and rotate the work, tied to the press by PLC and SCADA. In: ingot cast, continuously cast or preformed. Out: bars, tubes, shafts, axles. India’s first, and the world’s second largest.
-
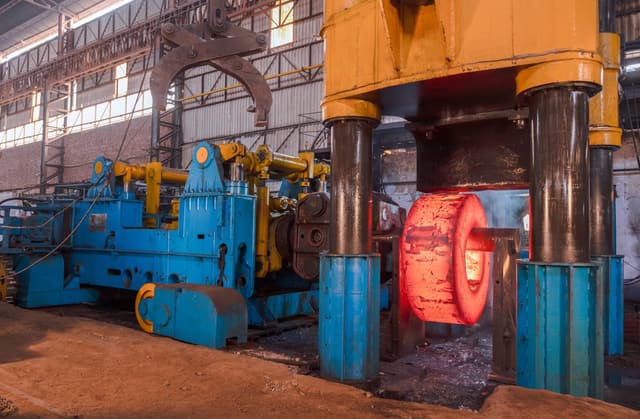
5,000 M.T. hydraulic forging press
Up to 3 m diameter
Paired with a 30 tonne-metre forging manipulator.
-
1,500 M.T. hydraulic forging press
Up to 1.2 m diameter
Paired with a 10 tonne-metre forging manipulator.
Furnaces
-
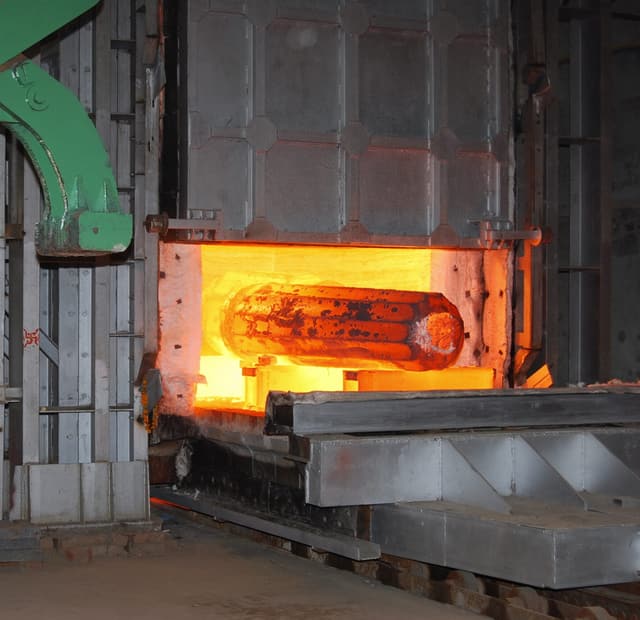
Gas-fired reheating furnaces
Up to 1400 °C
Multiple furnaces, each fitted with recuperators that recover heat from the exhaust gas.
-
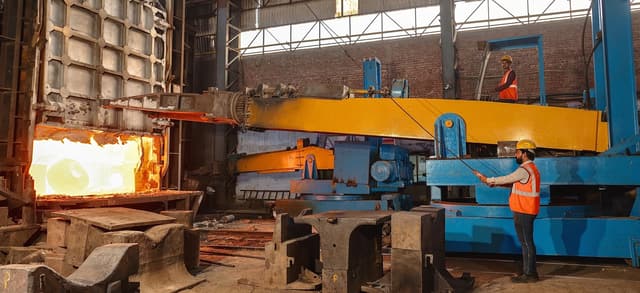
Rail-bound loading / unloading manipulators
2 units
Charge and draw the furnace without letting the ingot stand and lose heat.
Heat treatment
Normalising, annealing, quenching and tempering, all in-house.
-
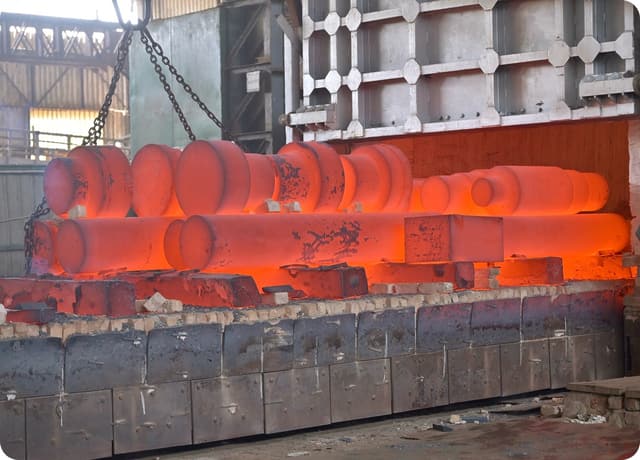
Gas-fired bogie-type furnaces
Up to 1200 °C
Multi-zone temperature monitoring, so a long shaft heats evenly along its length.
-
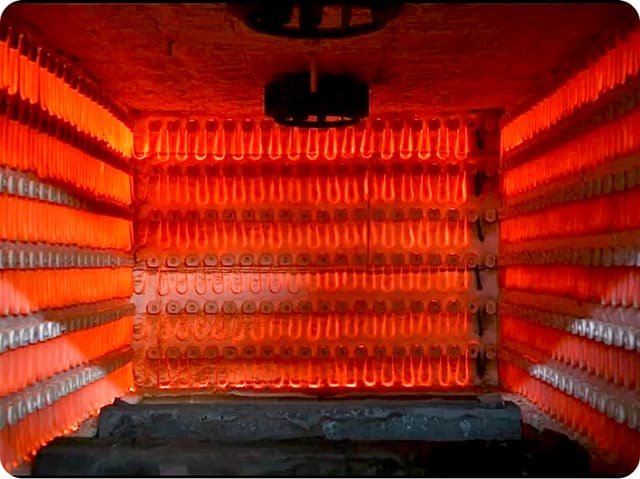
Electrical tempering furnaces
Up to 800 °C
Stable, closely controlled low-temperature cycles after quenching.
-
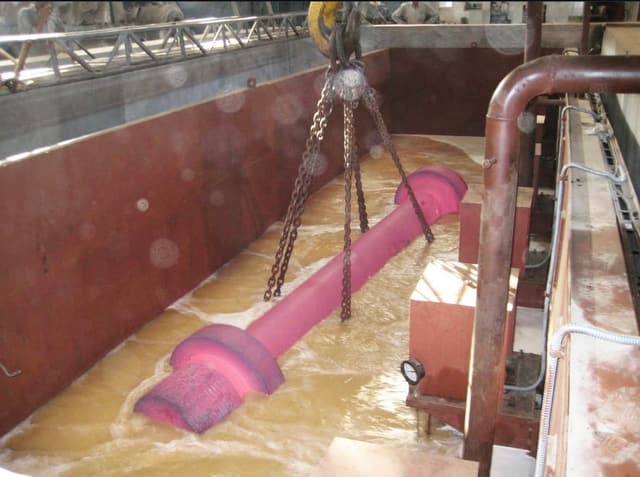
Polymer quench tank
2.5 × 3.5 × 9 m
Quench severity is adjustable, which is how the hardness and toughness are balanced against each other.
-
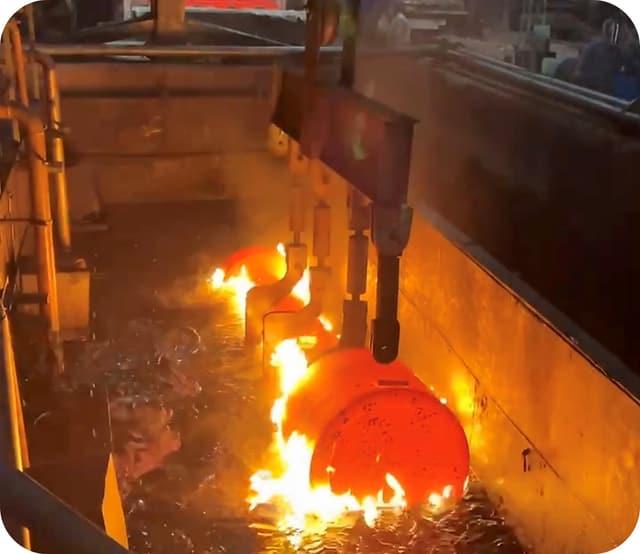
Oil quench tank
2.5 × 3.5 × 9 m
Uniform cooling, less distortion.
Machining
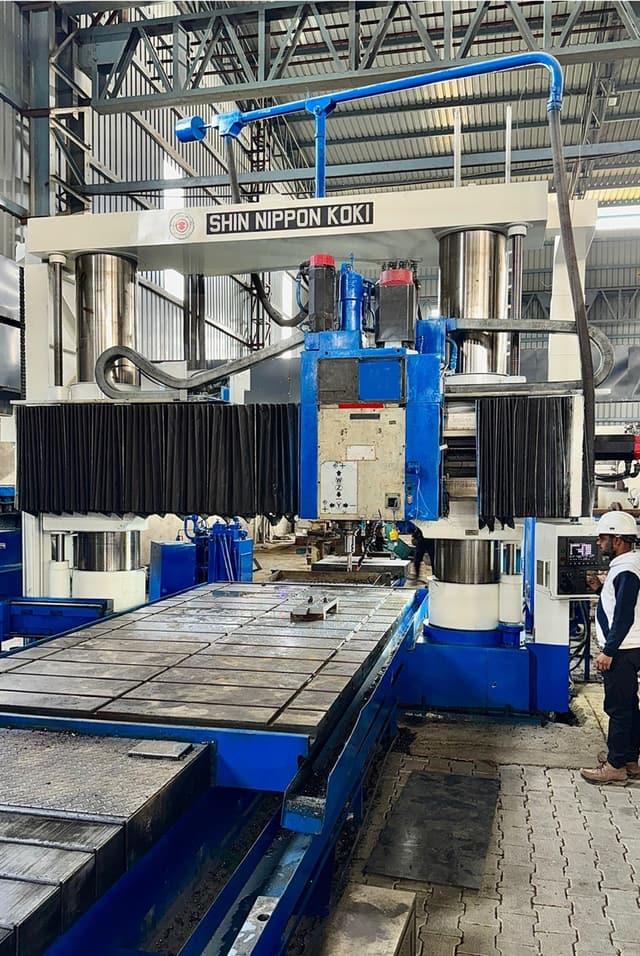
More than 90 large-capacity CNC machines, supported by a conventional machine fleet.
| Type | CNC | Manual | Envelope |
|---|---|---|---|
| Lathes | 28 | 25 | Ø 1,200 mm × 16,000 mm |
| Vertical turning lathes | 5 | 10 | Ø 5,000 mm × 3,000 mm height |
| Horizontal / vertical machining centres | 16 | 8 | 3 m W × 12 m L × 2.5 m H |
| Grinders | 2 | 7 | Ø 1,100 mm × 10 m |
| Deep-hole drills, hydraulic | 6 | — | 1,200 mm swing × 10 m |
| Radial drills | 4 | — | 2 m swing × Ø 65 mm |
| Tapping machines | 5 | — | Up to M48 |
Also available: cylindrical grinding, precision boring, milling and drilling.
A single integrated site
All of the above is located at our Pilkhuwa works. A part is cast, forged, heat treated, machined and packed without leaving the site.
-
Plant
Khasra 225/226, Masota Road, LakhanPilkhuwa, HapurUttar Pradesh, IndiaMelting shop, radial forge and CNC machine shop.
Send us your drawing
Tell us the shape, grade and quantity, and you will receive a reference number immediately.